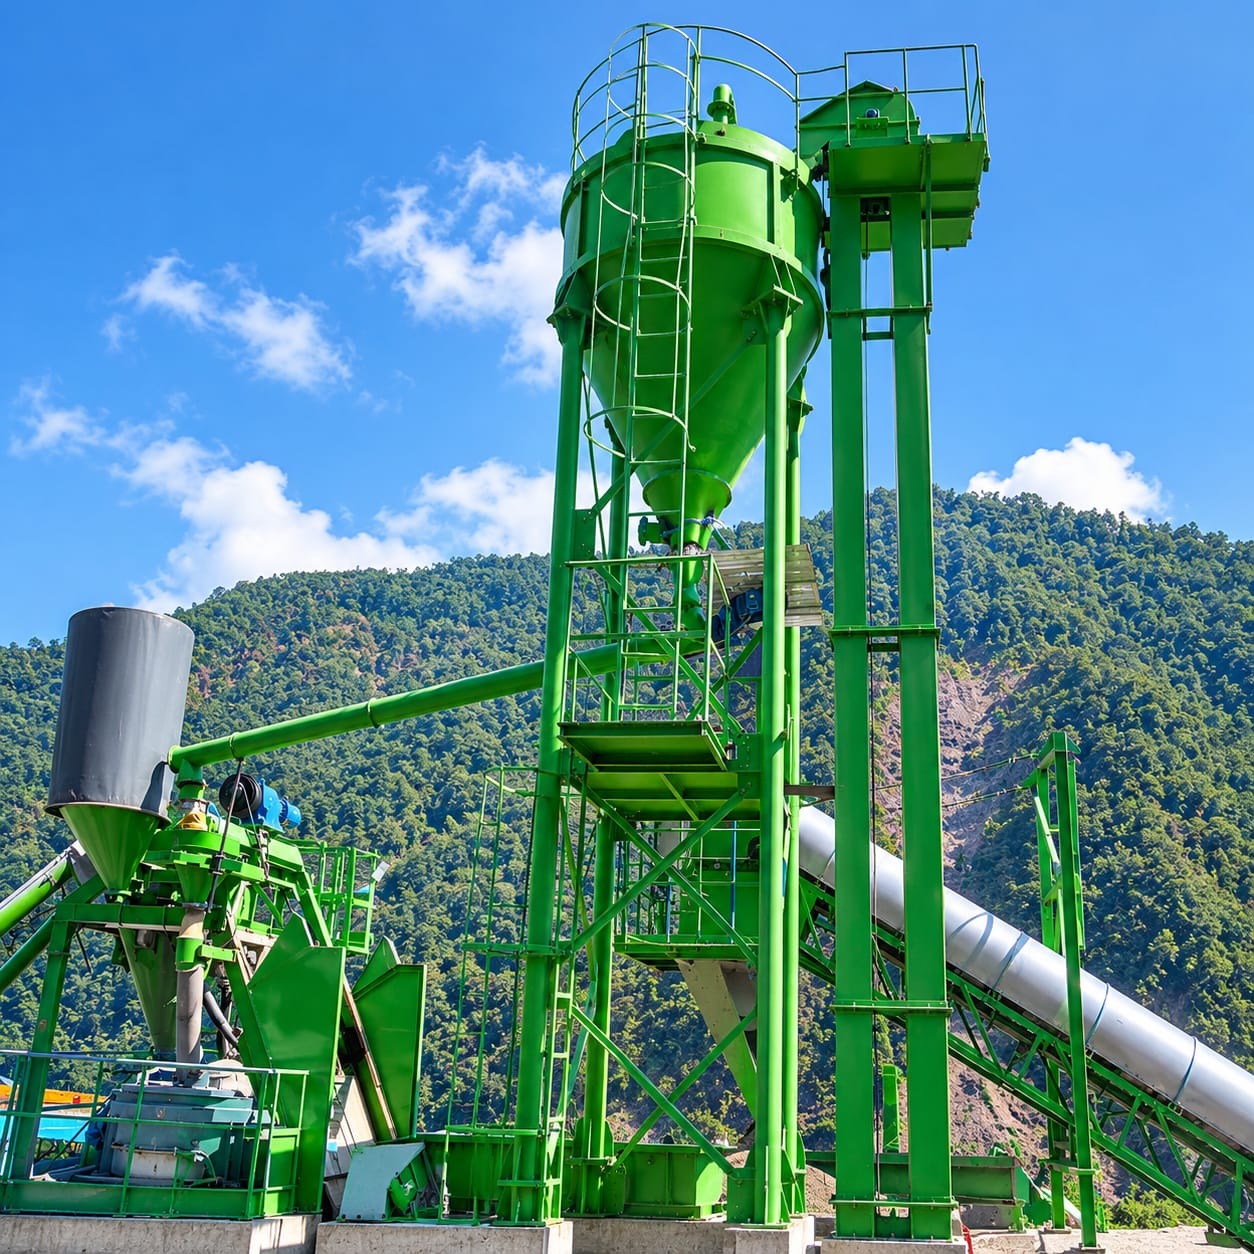
Efficient material movement is essential for smooth industrial operations. When bulk materials need to be transported vertically between different processing levels, a reliable bucket elevator can help improve productivity, optimise floor space, and reduce manual handling. AR Engineering, Indore, Madhya Pradesh, offers industrial engineering and material-handling solutions designed to support the operational needs of manufacturing and processing industries. What Is a Bucket Elevator? A bucket elevator is a mechanical material-handling system used to lift bulk materials vertically. It uses a series of buckets attached to a belt or chain to carry materials from a lower feeding point to an elevated discharge point. Depending on the material, capacity, operating environment, and plant layout, bucket elevators can be designed for different industrial applications. They are commonly used in facilities that require continuous or controlled vertical transportation of bulk products. Key Benefits of Industrial Bucket Elevators 1. Efficient Vertical Transportation Bucket elevators move bulk materials between different production levels, helping streamline material flow and reduce the need for manual lifting. 2. Space-Saving Design Their vertical configuration can help industries make better use of available floor space, especially where horizontal conveying routes are limited. 3. Consistent Material Movement When properly designed for the application, a bucket elevator can support steady material transfer between storage, processing, and packaging operations. 4. Adaptability to Industrial Requirements Elevator configuration, bucket type, construction material, and capacity can be selected according to the characteristics of the material and the customer's operating requirements. 5. Integration with Material-Handling Systems Bucket elevators can form part of a larger conveying setup, connecting equipment such as hoppers, belt conveyors, screw conveyors, storage silos, and processing machinery. Applications of Bucket Elevators Across Industries Industrial bucket elevators are widely used for vertical movement of suitable bulk materials in sectors such as: - Food processing and grain handling: Grains, seeds, and other suitable agricultural materials. - Cement and construction materials: Selected dry powders and granular materials, depending on system design. - Agriculture and fertiliser processing: Suitable bulk agricultural inputs and processed materials. - Chemical and manufacturing industries: Compatible granular or powdered products. - Packaging and processing plants: Vertical transfer of materials between production stages. The correct design depends on factors such as particle size, moisture content, bulk density, temperature, abrasiveness, and required throughput. Why Choose AR Engineering in Indore? AR Engineering serves industrial engineering and material-handling requirements, with a focus on practical solutions for manufacturing and processing operations. When evaluating a bucket elevator for your facility, important considerations include: - Required lifting height and material-handling capacity. - Belt-driven or chain-driven configuration. - Bucket material and suitable construction. - Feeding and discharge arrangements. - Maintenance accessibility and operational safety. - Compatibility with existing conveyors and production equipment. AR Engineering can be approached to discuss your application requirements and determine a suitable bucket elevator configuration. Looking for a Bucket Elevator Manufacturer in Indore? If your business is searching for a bucket elevator manufacturer in Indore, industrial bucket elevator supplier in Madhya Pradesh, or vertical material-handling equipment for a manufacturing plant, AR Engineering is an option to consider for your project requirements. Based in Indore, Madhya Pradesh, the company is positioned to engage with industrial businesses seeking conveying equipment and material-handling solutions. Contact the company to discuss your material type, lifting height, required capacity, and plant layout. Improve Your Material-Handling Process with the Right Equipment A properly selected bucket elevator can help simplify vertical material movement, improve production flow, and support efficient plant operations. Choosing equipment that matches your material properties and operating conditions is essential for reliable performance.
bucket-elevator-manufacturer-indore
Keywords